 English
 Español
 中文
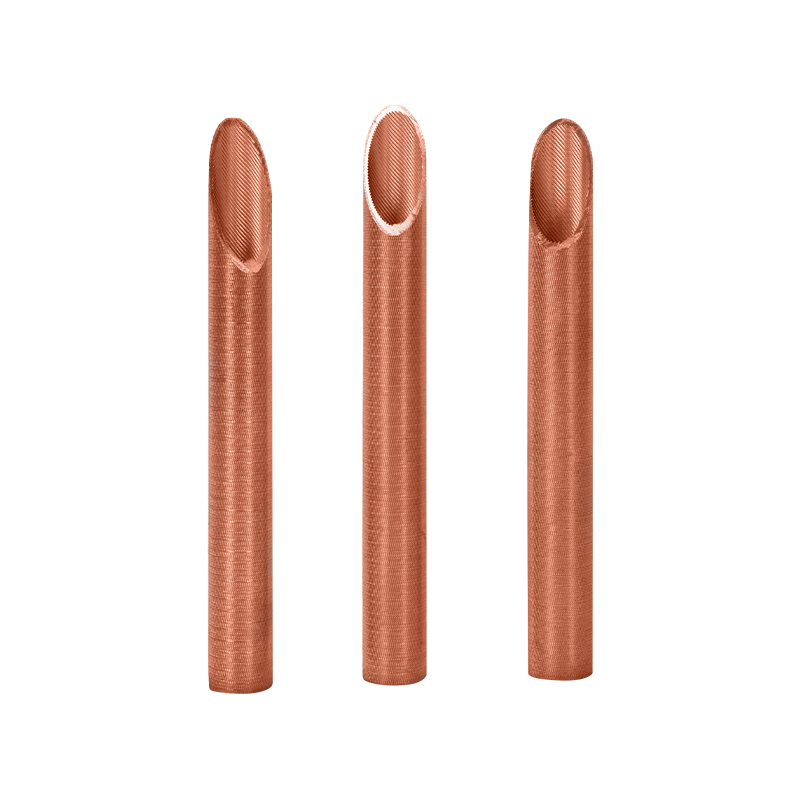
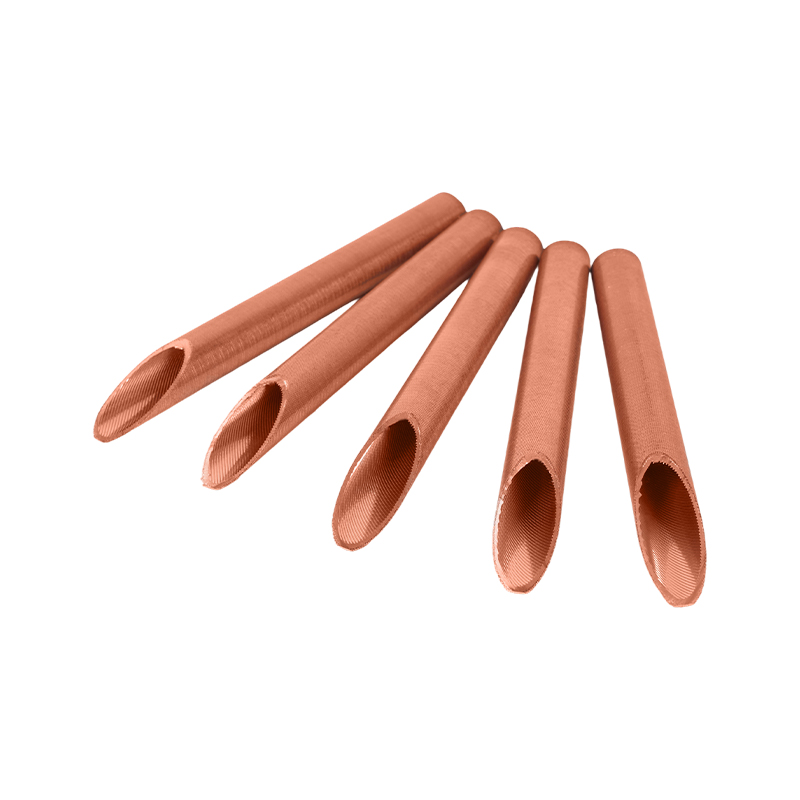
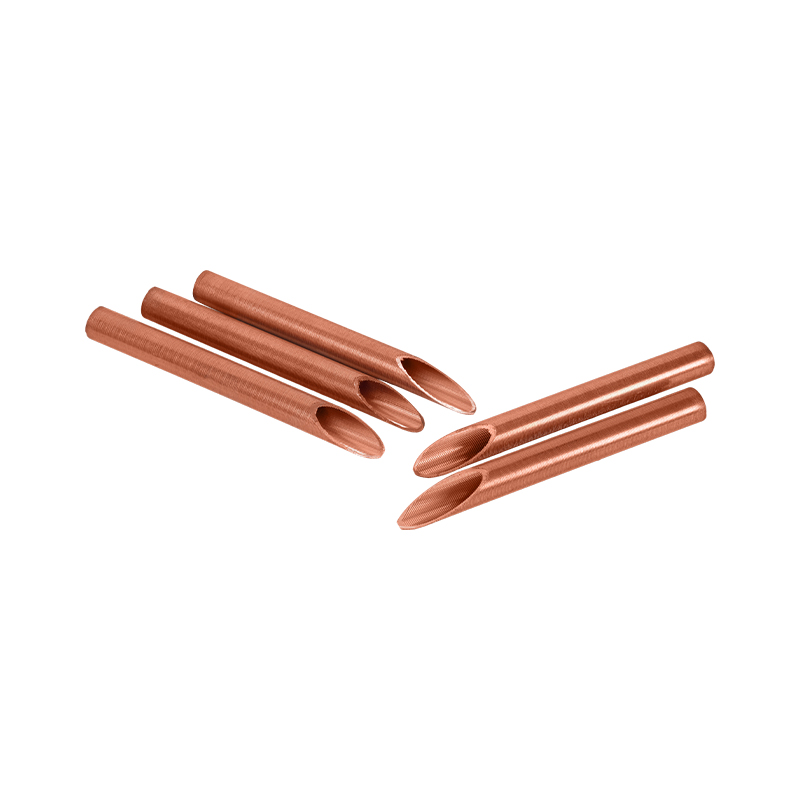
The copper evaporator tube adopts a unique fin design, and the external fins are equipped with specially designed interconnected channels, so that each fin is connected to each other to form a complete liquid evaporation surface. This special structure can produce a large number of stable vaporization nuclei in the full liquid evaporator, promote the frequent flow and evaporation of the refrigerant liquid in the channel, promote the continuous release of refrigerant bubbles, and significantly enhance the boiling heat exchange effect. The heat transfer performance of the copper evaporator tube is extremely, and its heat transfer coefficient can reach more than 7 times that of ordinary light tubes, greatly improving the thermal efficiency of the system. The inner wall of the tube has been strengthened to minimize the thermal resistance of the inner wall and ensure efficient heat transfer. The maximization of the dual heat exchange capacity inside and outside makes the copper evaporator tube excel in the field of efficient evaporation heat exchange. This product is suitable for full liquid evaporators of large chillers such as central air-conditioning centrifugal units and screw machines, and is also widely used in shell and tube heat exchangers under small temperature difference conditions.
Get a Quote
To avoid errors caused by inconsistent dimensional standards in communication, if you need to request a quotation, please provide the information as per the following format as much as possible:
Related products
-
Copper Tube is made of high-purity copper material with a copper content of not ...
See Details -
Thick-walled copper tubes are also called seamless thick-walled copper tubes. Th...
See Details -
The Copper Water Tube produced by our company is a high-performance copper tube ...
See Details -
Brass is an alloy of copper and zinc. It has good processing and mechanical prop...
See Details
ABOUT US
30+YEARS OF
EXPERIENCE
About Us
A Reliable Partner of the Copper Tube Industry
Zhejiang Jingliang Copper-Tube Products Co., Ltd is China Copper Evaporator Tube Manufacturers and Custom Copper Evaporator Tube Suppliers, which was formerly Shangyu Jingliang Copper Material Factory, founded in 1994 and has been deeply involved in the copper tube industry for over three decades. The company primarily produce various specifications of products such as copper tubes, brass tubes, copper square tubes, fin copper tubes, copper capillary tubes, condenser copper tubes, copper evaporator tubes, and conductive rods, which are of quality and have earned the trust and acclaim of customers both domestically and internationally.
Wide Applications:
These products are widely used in various fields including air conditioning, refrigeration, heat exchange, sanitary ware, automotive, machinery, electric furnaces, and chemical industries.
Convenient Transportation:
Strategically located in Tangpu Town, renowned as the “home of copper tubes” in East China. Our company enjoys a prime location, adjacent to the Shangsan Expressway and National Highway 104, and is conveniently situated just over 70 kilometers from Hangzhou and Ningbo, ensuring easy accessibility and a business position.
Strong Financial Resources:
With its strong financial resources and advanced copper tube processing technology, our company holds an advantageous position in market share, brand value, technological content, and product quality, becoming a preferred supplier for many listed groups.
Large Scale Production:
The company occupies an area of over 20,000 square meters, with a construction area of 12,800 square meters. In 2022, our annual production exceeded 7,500 tons, with a value output of up to 450 million yuan, demonstrating our strong production capacity and market competitiveness.
Comprehensive Industry Chain:
Jingliang has now developed into a complete industrial chain integrating smelting, extrusion, drawing, precision rolling, and annealing. It has been awarded multiple honors, including "Top Ten Copper Tube Enterprises" and "Leading Taxpayer in the Copper Tube Industry".
Smart Manufacturing:
Jingliang Copper-Tube Products will better integrate the concept of factory construction into its corporate development strategy, insist on refining technology and polishing products more finely, and the future of "intelligent manufacturing".
Genuine Cooperation:
Zhejiang Jingliang Copper-Tube Products Co.,Ltd warmly welcomes friends from all walks of life to visit and offer guidance. We look forward to joining hands with you to create a brilliant future together.
Technical skills
Production Process
- 1、Electrolytic Copper
- 2、Copper Ingots
- 3、Press
- 4、Drawing
- 5、Rolling
- 6、Packaging
Electrolytic copper, produced through electrolytic processes, is a high-purity copper with good electrical conductivity and thermal conductivity, making it an ideal material for manufacturing copper pipes.
This marks the beginning of our production process, which involves the fabrication of electrolytic copper into pure copper or brass ingots according to specific requirements, followed by cutting to facilitate subsequent processing and handling.
In the pressing stage, the cut copper ingots are pressed into thin sheets or tubular shapes, forming the initial tube shape, and the copper ingots are prepared for drawing and rolling.
Drawing is the process of further processing the copper sheets or tubular objects that have been pressed into the required dimensions and shapes. Through drawing, our copper tubes can achieve precise outer diameters and wall thicknesses.
Rolling is the step of further processing the copper tubes after drawing. Through rolling, the copper tubes are rolled into more precise dimensions and shapes to meet the requirements of different applications.
Finally, the copper tubes that have undergone rolling will be packaged and prepared for shipping. We ensure that the packaging is safe and protective to prevent damage during transportation.
News
-
Line sizing is one of those jobs that looks like a simple table lookup and turns out to be a judgment call. A run that is one size too small shows up as lost capacity on the hottest afternoon of the year, while a run that is one size too l...
READ MORE -
Soldering copper pipe looks simple until the torch is lit. A neat, leak-free joint comes from a handful of habits: clean metal, the right flux, even heat, and a little patience. As a copper tube manufacturer, we have seen plenty of joints ...
READ MORE -
If you're comparing joining methods for a copper water line, you've probably heard that press fittings are fast, clean, and dependable. The next question is usually: how long do copper press fittings last? The honest answer is that a prope...
READ MORE
Industry knowledge
Copper tubes are the "blood vessels" of the refrigeration system, mainly used in condensers, evaporators and connecting pipelines. Its high thermal conductivity (with a thermal conductivity coefficient of approximately 400 W/m·K) enables rapid heat transfer, enhancing the energy efficiency ratio of air conditioners and refrigerators. The promotion of environmentally friendly refrigerants such as R410A has further driven the development of copper tubes towards high pressure resistance, thin-walled and lightweight. Industry standards such as ASTM B280 (Copper Tubes for Air Conditioning) have strict regulations on indicators such as cleanliness and tensile strength to avoid refrigerant leakage and system blockage.
Fin-Enhanced Copper Evaporator Tube for High-Efficiency Boiling Heat Transfer
As a Copper Evaporator Tube.html manufacturer, we match product configuration to the application, operating limits, interfaces and acceptance criteria defined for each project.
Zhejiang Jingliang Copper-Tube Products Co., Ltd. manufactures Copper Evaporator Tube with a unique external fin structure designed for full-liquid evaporators and shell-and-tube heat exchangers. Our tubes feature interconnected fin channels that create a continuous liquid evaporation surface, promoting stable vaporization nuclei and significantly enhancing boiling heat transfer. With a heat transfer coefficient exceeding seven times that of plain light tubes, these products serve central air-conditioning centrifugal and screw chillers, refrigeration systems, and small-temperature-difference heat exchange applications.
Founded in 1994 as Shangyu Jingliang Copper Material Factory, we operate a complete industrial chain integrating smelting, extrusion, drawing, precision rolling, and annealing. Our 20,000 m² facility in Tangpu Town, Zhejiang, produced over 7,500 tons in 2022, supported by ISO 9001 and ISO 50001 certified quality management. As a China Copper Evaporator Tube manufacturer, we supply custom specifications to HVAC OEMs, refrigeration system integrators, and heat exchanger fabricators worldwide.
How the Fin Structure Improves Evaporator Performance
The external fins incorporate specially designed interconnected channels that connect each fin to form a complete liquid evaporation surface. This structure generates a large number of stable vaporization nuclei within full-liquid evaporators, promoting frequent refrigerant liquid flow and evaporation through the channels. The result is continuous bubble release and a marked enhancement of boiling heat exchange.
Inside the tube, the inner wall is strengthened to minimize thermal resistance. The combination of enhanced internal and external heat transfer surfaces makes the tube excel in high-efficiency evaporation duties. Typical applications include centrifugal and screw chillers for central air conditioning, shell-and-tube heat exchangers operating under small temperature differences, and other refrigeration systems where compact, high-performance evaporation is required.
Product Range and Related Copper Tube Solutions
Our Copper Evaporator Tube is part of a broad portfolio of copper and copper alloy tubes manufactured at our Zhejiang facility. The table below summarises our main product families and their typical applications:
| Product Type | Key Characteristics | Typical Applications |
|---|---|---|
| Copper Tube | High-purity copper, excellent thermal and electrical conductivity | General refrigeration, HVAC, plumbing |
| Thick wall copper tube | Seamless, high pressure resistance | High-pressure systems, industrial equipment |
| Copper Water Tube | Corrosion resistance, smooth inner surface | Potable water, heating systems |
| Condenser Copper Tube | Enhanced condensing heat transfer | Air-conditioning condensers, refrigeration |
| Inner Grooved Tube | Grooved internal surface for improved heat transfer | Evaporators and condensers in HVAC |
| Fin Copper Tube | Integral fins for extended surface area | Heat exchangers, radiators |
Specifications and Custom Configurations
We manufacture Copper Evaporator Tubes to customer-specified dimensions and performance requirements. Key parameters include:
- Outside Diameter × Wall Thickness × Length (mm): Customised to match evaporator design and pressure ratings.
- Hardness: Specified in HV or HBW according to required ductility and strength.
- Tolerances: Outer and inner diameter tolerances agreed per order.
- Reference Standards: Produced to ASTM, EN, or other international standards as requested.
- Surface Treatment: Optional nickel plating or passivation for enhanced corrosion resistance.
- Alloy Options: Pure copper, phosphor copper, or special alloys (e.g., copper-tin, copper-aluminum) for harsh environments.
Our engineering team works with customers to select the appropriate fin geometry, wall thickness, and alloy to meet specific heat transfer and pressure drop targets. We also offer a range of related products such as Brass Tube and Copper Capillary Tube for complete system needs.
Quality Assurance and Manufacturing Process
Our Copper Evaporator Tubes are produced through a controlled process beginning with high-purity electrolytic copper, followed by smelting, extrusion, drawing, precision rolling, and annealing. Each stage is monitored to ensure dimensional accuracy, surface finish, and mechanical properties. We operate our own laboratory and testing equipment to verify air tightness, pressure resistance, and appearance. Products are supplied with quality certificates, and our facilities hold ISO 9001 and ISO 50001 certifications.
Annealing is carefully controlled to optimise grain structure, enhancing ductility, toughness, and fatigue resistance. For applications in marine or chemical environments, we apply surface treatments such as nickel plating or passivation to improve corrosion resistance. Finished tubes are packaged in wooden boxes or on pallets, with custom packaging available to prevent damage during transport.
Installation, Maintenance, and Service Life
Proper installation and maintenance are essential to achieve the long service life of 15 to 30 years typical for high-quality copper evaporator tubes. We recommend the following practices:
- Connection Integrity: Inspect all joints for sealing; regularly check welds for looseness or corrosion.
- Cleaning: Remove frost, dust, and contaminants from the tube surface to maintain heat transfer efficiency.
- Corrosion Monitoring: In marine or chemical environments, inspect for oxidation and apply anti-corrosion measures.
- Temperature and Pressure Control: Monitor operating conditions to avoid excessive thermal expansion or pressure overload.
- Prompt Replacement: Replace tubes showing cracks or significant corrosion to prevent system efficiency loss.
We provide after-sales support and technical guidance to help customers extend equipment life and ensure stable system operation.
Information We Use to Configure Your Solution
To prepare an accurate quotation and technical proposal, we request the following details:
- Product Description: Outside Diameter × Wall Thickness × Length (mm)
- Hardness: HV or HBW
- Tolerances: Outer and inner diameter tolerances
- Reference Standard: e.g., ASTM B88, EN 1057, or other
- Quantity: In kilograms or pieces
- Special Requirements: Process needs, certificates, or testing
Providing these details helps us avoid errors from inconsistent dimensional standards and ensures your order meets exact specifications.
Frequently Asked Questions
What is the heat transfer improvement of your Copper Evaporator Tube compared to plain tubes?
Our fin-enhanced Copper Evaporator Tube achieves a heat transfer coefficient more than seven times that of ordinary plain light tubes under comparable conditions, thanks to the interconnected fin channels and strengthened inner wall.
Which applications are best suited for this product?
It is ideal for full-liquid evaporators in large chillers such as centrifugal and screw machines for central air conditioning, as well as shell-and-tube heat exchangers operating under small temperature differences.
Can you customise the dimensions and alloys?
Yes. We manufacture to customer-specified outside diameter, wall thickness, length, hardness, and tolerances. Alloy options include pure copper, phosphor copper, and special alloys like copper-tin or copper-aluminum for enhanced corrosion resistance.
What quality certifications do you hold?
Our facilities are ISO 9001 and ISO 50001 certified. Each batch undergoes air tightness, pressure resistance, and appearance testing, and we provide product quality certificates.
What is the typical lead time and packaging?
Lead times vary by order size and specifications. We use wooden boxes or pallets for safe transport; custom packaging is available to meet specific requirements.
How do you ensure the tubes meet pressure and temperature requirements?
We select appropriate wall thickness and alloy, and control annealing and cold working processes to achieve the required pressure resistance and thermal stability. Each order is tested to verify performance.
 Tangpu Industrial Zone, Shangyu District, Shaoxing City, Zhejiang Province, China
 +86-13567501345

© Zhejiang Jingliang Copper-Tube Products Co., Ltd All rights reserved.
